How Preheating and Cooling Zones Affect Tunnel Kiln Performance

Understanding how a tunnel kiln preheating zone interacts with firing and cooling stages is critical for buyers specifying continuous kilns. This guide explains the functional roles of preheating and cooling zones, how they affect throughput, product quality and energy use, and what to put in an RFQ to validate claims.
The exact effects on a given production line depend on product geometry, load arrangement, insulation strategy and control systems. Use the practical checks below to compare vendor options and to prepare site-specific tests and acceptance criteria before purchase.
Why the tunnel kiln preheating zone matters
The tunnel kiln preheating zone conditions incoming green or damp products before they enter the high-temperature firing region. A well-designed preheating zone reduces thermal shock, controls moisture removal and improves energy transfer into the main firing profile. These outcomes influence product integrity and downstream yield.
Independent guidance recommends evaluating preheating within the full kiln system — not as an isolated module — because preheating performance interacts with insulation, firing curve, airflow patterns and cooling-air recovery strategies [1][2].
How preheating and cooling zones interact
Preheating and cooling are two sides of the same thermal balance. Heat recovered from the cooling zone can be reused in the preheating zone if airflow and ducting are designed for heat recovery. Properly matched zones stabilize firing curves and can reduce net fuel consumption when implemented correctly; independent studies stress evaluating heat recovery, airflow direction and stack stability as part of overall project assessment [1][2].
Key design elements to evaluate
- Airflow paths and separation between process gases and combustion gases.
- Insulation and refractory continuity between zones to limit unwanted heat loss.
- Control of moisture removal rate to avoid cracking or blistering of products.
- Integration of heat recovery from cooling air to the preheating zone.
- Modularity and maintainability of the kiln body and zone components.
Supplier statements vs independent considerations
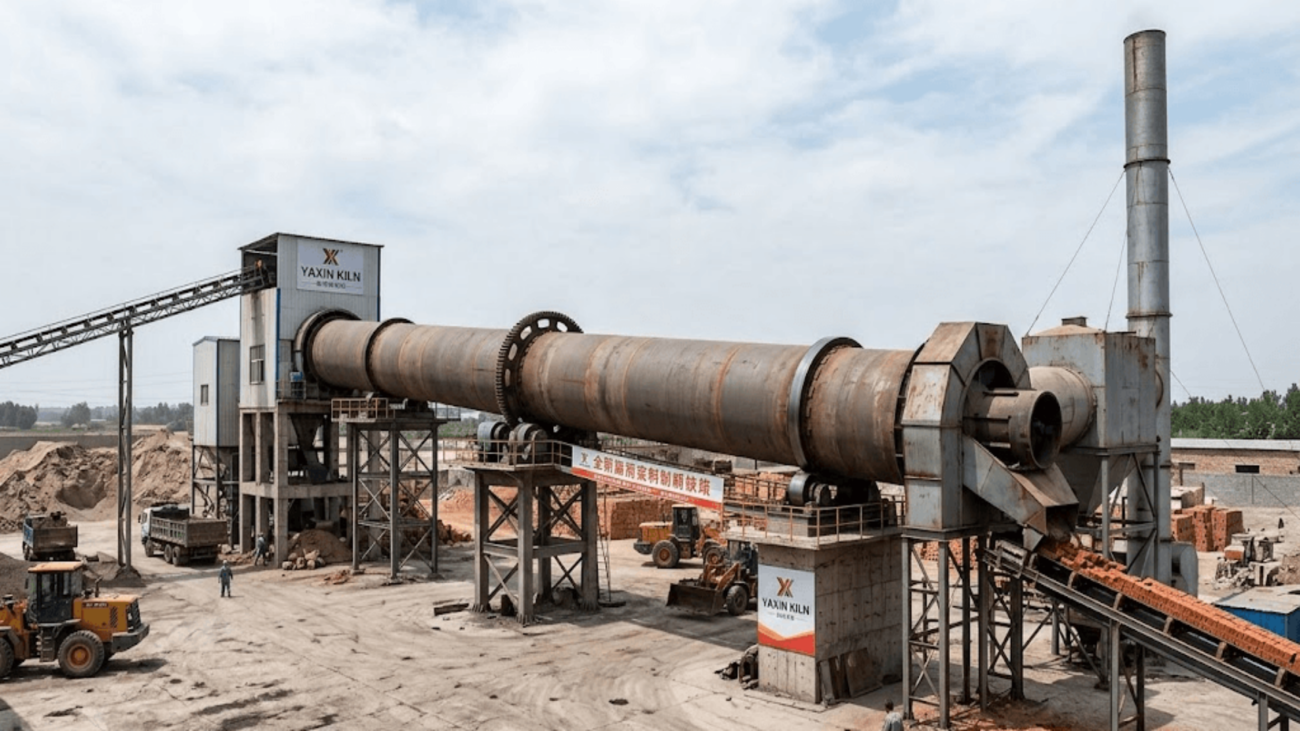
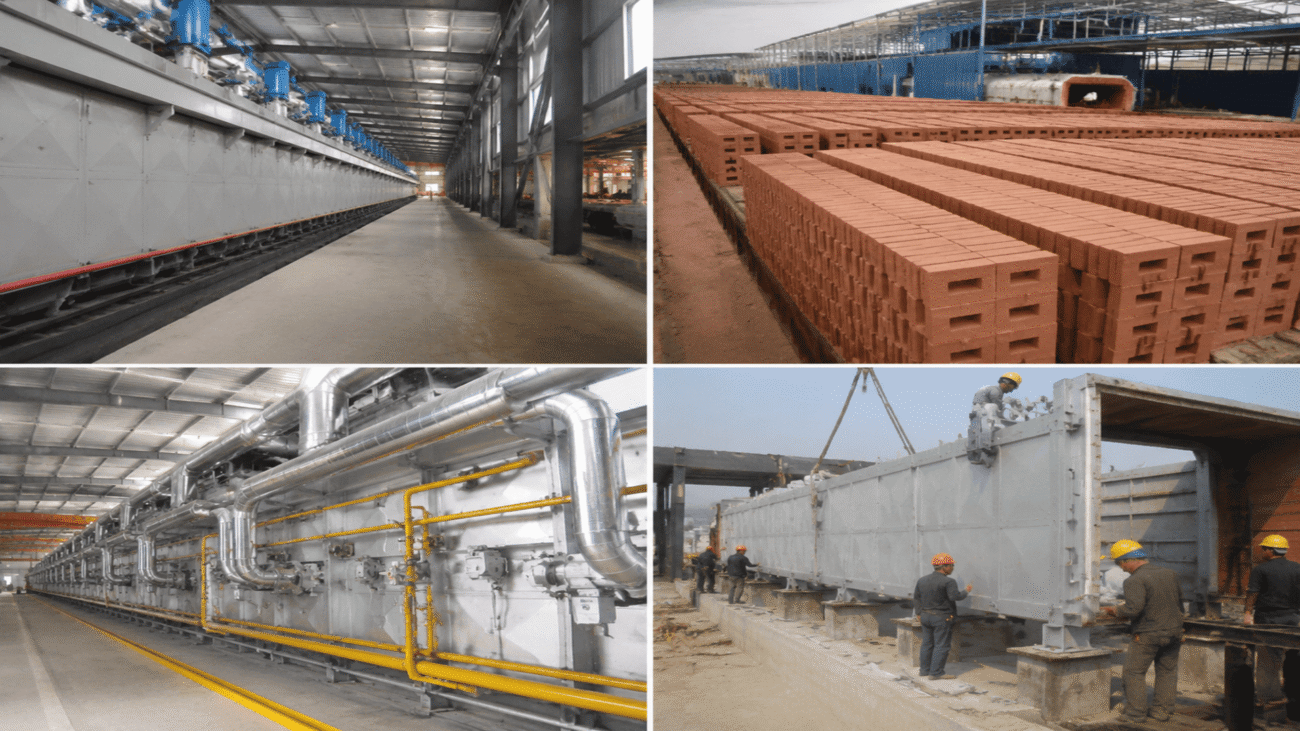
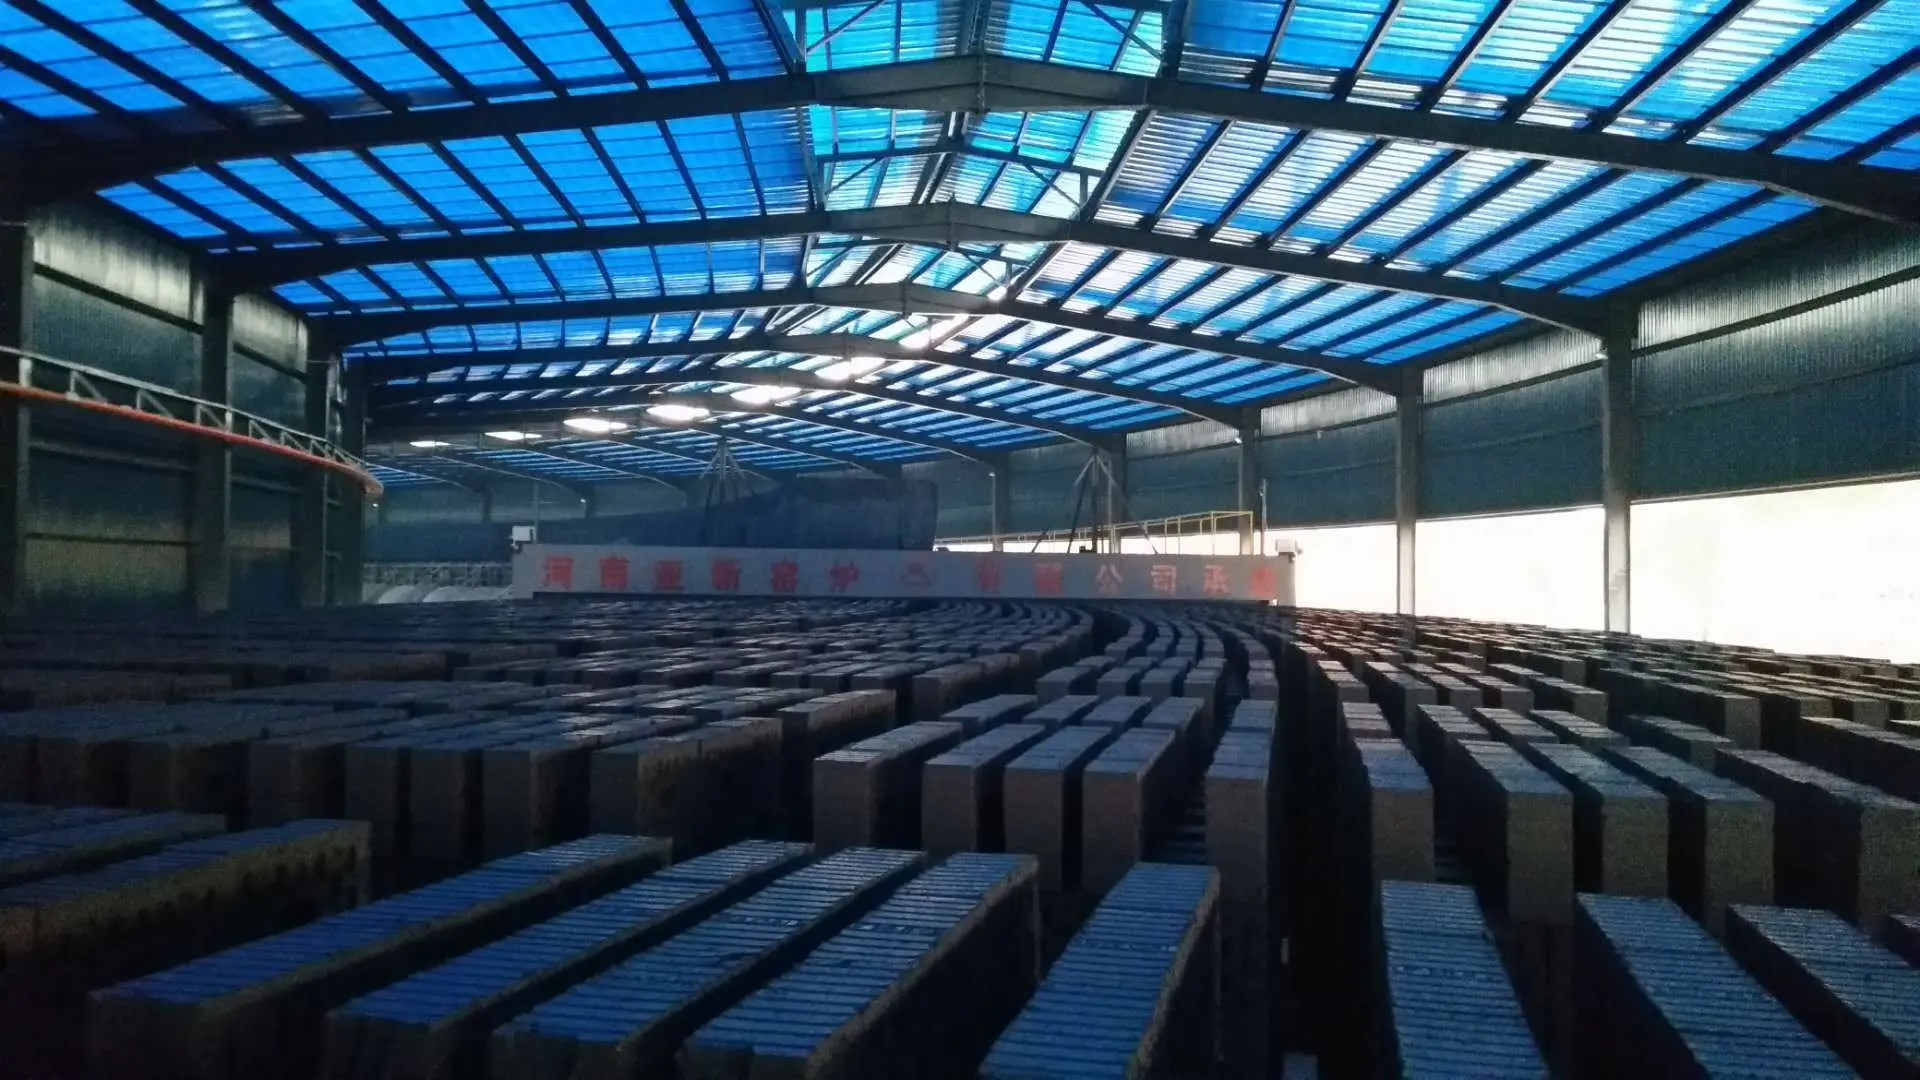
Supplier product pages may list design features and intended benefits. For example, Yaxin Kiln describes a prefabricated tunnel-kiln body with modular assemblies, multiple tracks, synchronous drying and roasting, double sealing, rapid drying, automation, and staged drying/preheating/calcining/insulation/cooling stages, plus flue-gas reburning and cooling-air recovery strategies [3]. Those are supplier statements about product capabilities and assembly approach.
Independent sources recommend treating such statements as part of a broader assessment that includes life-cycle considerations, fuel and emissions performance, and operational productivity estimates [1]. Thermal-analysis studies show that product geometry, load flow and temperature gradients drive quality outcomes and must be modelled or tested for each application [2].
Comparison table: decision points for preheating and cooling design
| Decision factor | Preheating focus | Cooling focus |
|---|---|---|
| Primary objective | Controlled moisture removal; gradual temperature ramp | Heat extraction; product stabilization and quenching control |
| Impact on quality | Reduces cracking and improves firing uniformity | Determines post-firing dimensional stability and surface finish |
| Energy strategy | Can accept recovered heat from cooling air | Source for heat-recovery loops if air flows are segregated |
| Control complexity | Requires moisture and temperature profiling | Requires staged airflow and heat-recovery control |
Operational checks and instrumentation
To evaluate real-world performance, specify measurements and instrumentation in the RFQ or test program: zone temperature profiles, humidity and moisture-removal rates, differential pressures between zones, and the temperature of recovered cooling air when applicable. Simulation and trial runs with instrumented loads are recommended to validate the firing curve and stack stability [2].
Integration, modularity and maintenance
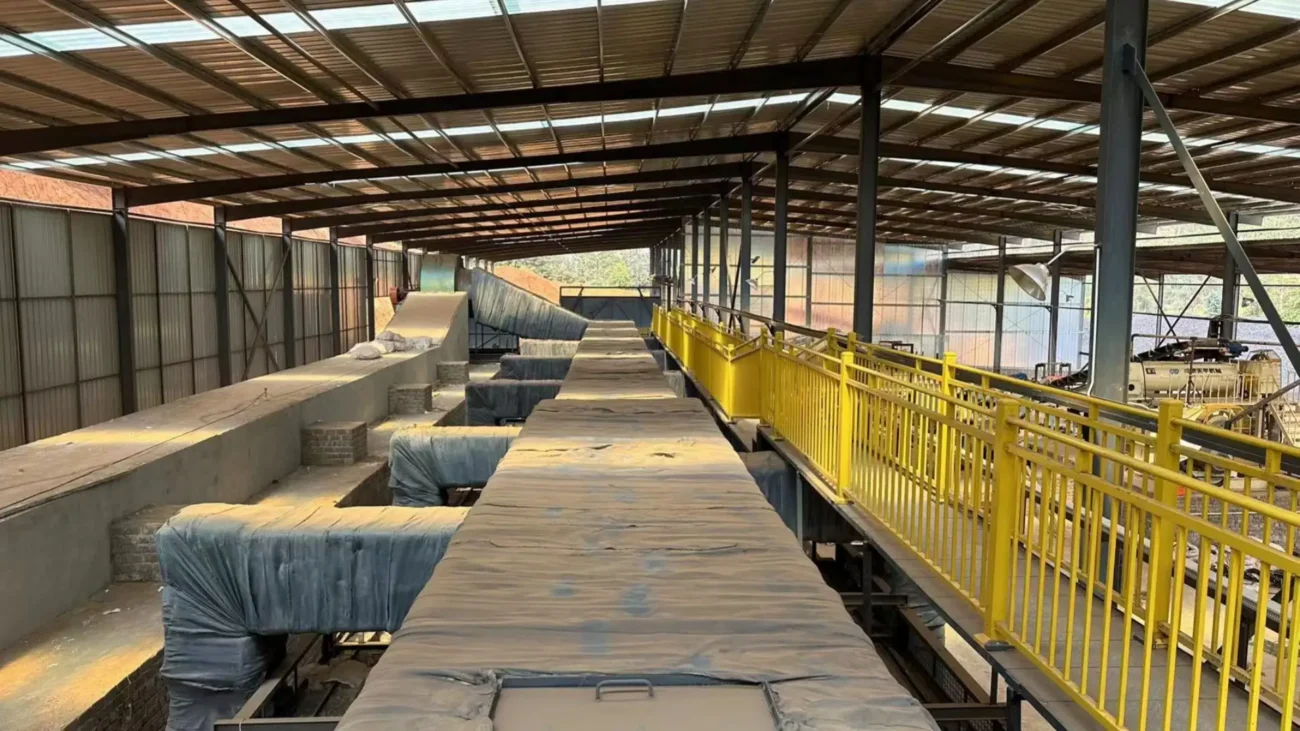
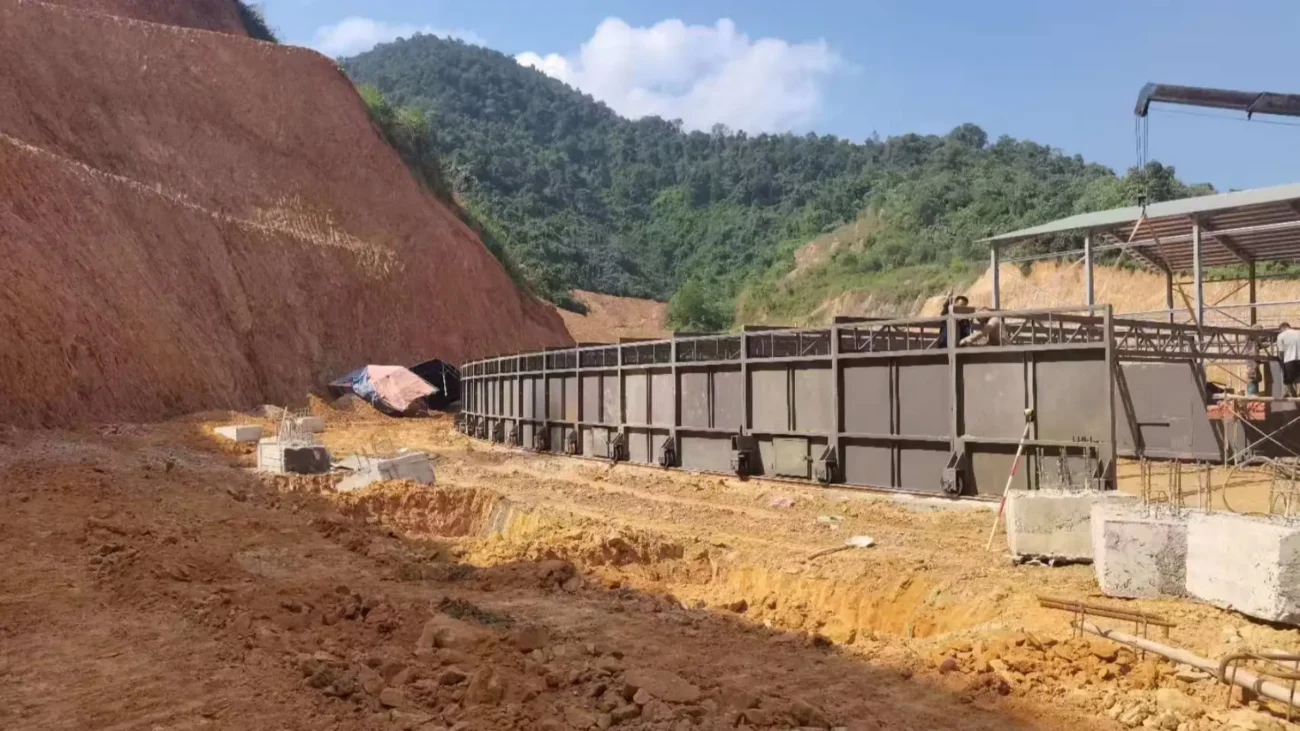
Modular zone assemblies simplify installation, alignment of multiple kiln-car tracks and future maintenance. Supplier descriptions that a kiln is prefabricated or modular indicate potential advantages for reduced site work; however, on-site assembly, sealing quality and alignment must be verified as part of acceptance testing [3].
When preheating design can reduce operating risk
Proper preheating reduces abrupt moisture gradients, lowering breakage and rework. It also helps standardize the heat-up portion of the firing curve so the firing zone sees a predictable inlet condition. Independent guidance recommends evaluating these benefits in a productivity versus operating-cost framework, considering fuel type, emissions and longevity of lining and refractory systems [1].
RFQ / validation checklist
| Checklist item | Buyer validation action |
|---|---|
| Site data | Provide floor plan, utilities, elevations, and ambient conditions |
| Product specs | Submit product dimensions, moisture content, and acceptable quality criteria |
| Trial requirements | Request instrumented test runs and performance reports |
| Heat recovery intent | Specify desired heat-recovery rate and testing method |
| Acceptance tests | Define temperature profiles, product yield and inspection criteria |
Practical troubleshooting tips
If moisture-related defects appear after installation, check preheating airflow uniformity, track alignment and sealing between zones. If firing variability appears, inspect insulation continuity and measure temperature gradients across the product load. Independent thermal analyses show that uneven airflow or insulation discontinuities are common root causes of quality problems [2].
Cost and lifecycle considerations
Independent project guidelines recommend evaluating preheating and cooling design alongside capital cost, operating fuel use and emissions, expected lining life and land use. Those assessments help balance upfront investment against long-term operating risk and regulatory concerns [1].
FAQs
How does preheating reduce product breakage?
Preheating moderates the rate of moisture removal and temperature rise, which reduces internal stresses from rapid evaporation. Proper zone control and airflow balance are needed to achieve this effect reliably [2].
Can cooling heat be reused for preheating?
Yes—if cooling air and process flue gases are segregated and ducted into heat-recovery systems, the recovered heat can be used in the preheating zone. Implementation requires controls to avoid cross-contamination of gases and to maintain zone temperature stability [1][3].
What should I require from suppliers in the RFQ?
Request documented zone temperature profiles, descriptions of airflow and sealing strategies, modular assembly details, proposed heat-recovery arrangements, and a test plan that includes instrumented trial runs with your products. Treat supplier claims as inputs to be validated by site testing and RFQ-confirmed acceptance criteria.
For details on a prefabricated modular approach and supplier-stated features, see the Yaxin Kiln prefabricated tunnel-kiln page for their stated capabilities and assembly approach [3]. To evaluate vendor proposals, pair supplier statements with independent thermal modelling and the operational checks described above.
When you’re ready to compare vendor designs, request modular assembly drawings, scope of on-site work, and instrumented trial schedules. For a supplier product page and contact information, review the prefabricated tunnel-kiln offering here: prefabricated tunnel-kiln.
RFQ-confirmation scope: final performance and operational outcomes must be confirmed by an RFQ process that specifies site data, material tests, load patterns, instrumented trial runs and clear acceptance criteria defined by the buyer and verified on-site.